
WIDIA - Полный каталог инструмента - 2017
Hole Finishing
Reamer Custom Solution Capabilities
для размещения заказа - zakaz@widiahanita.ru
Reamer Troubleshooting
Problem
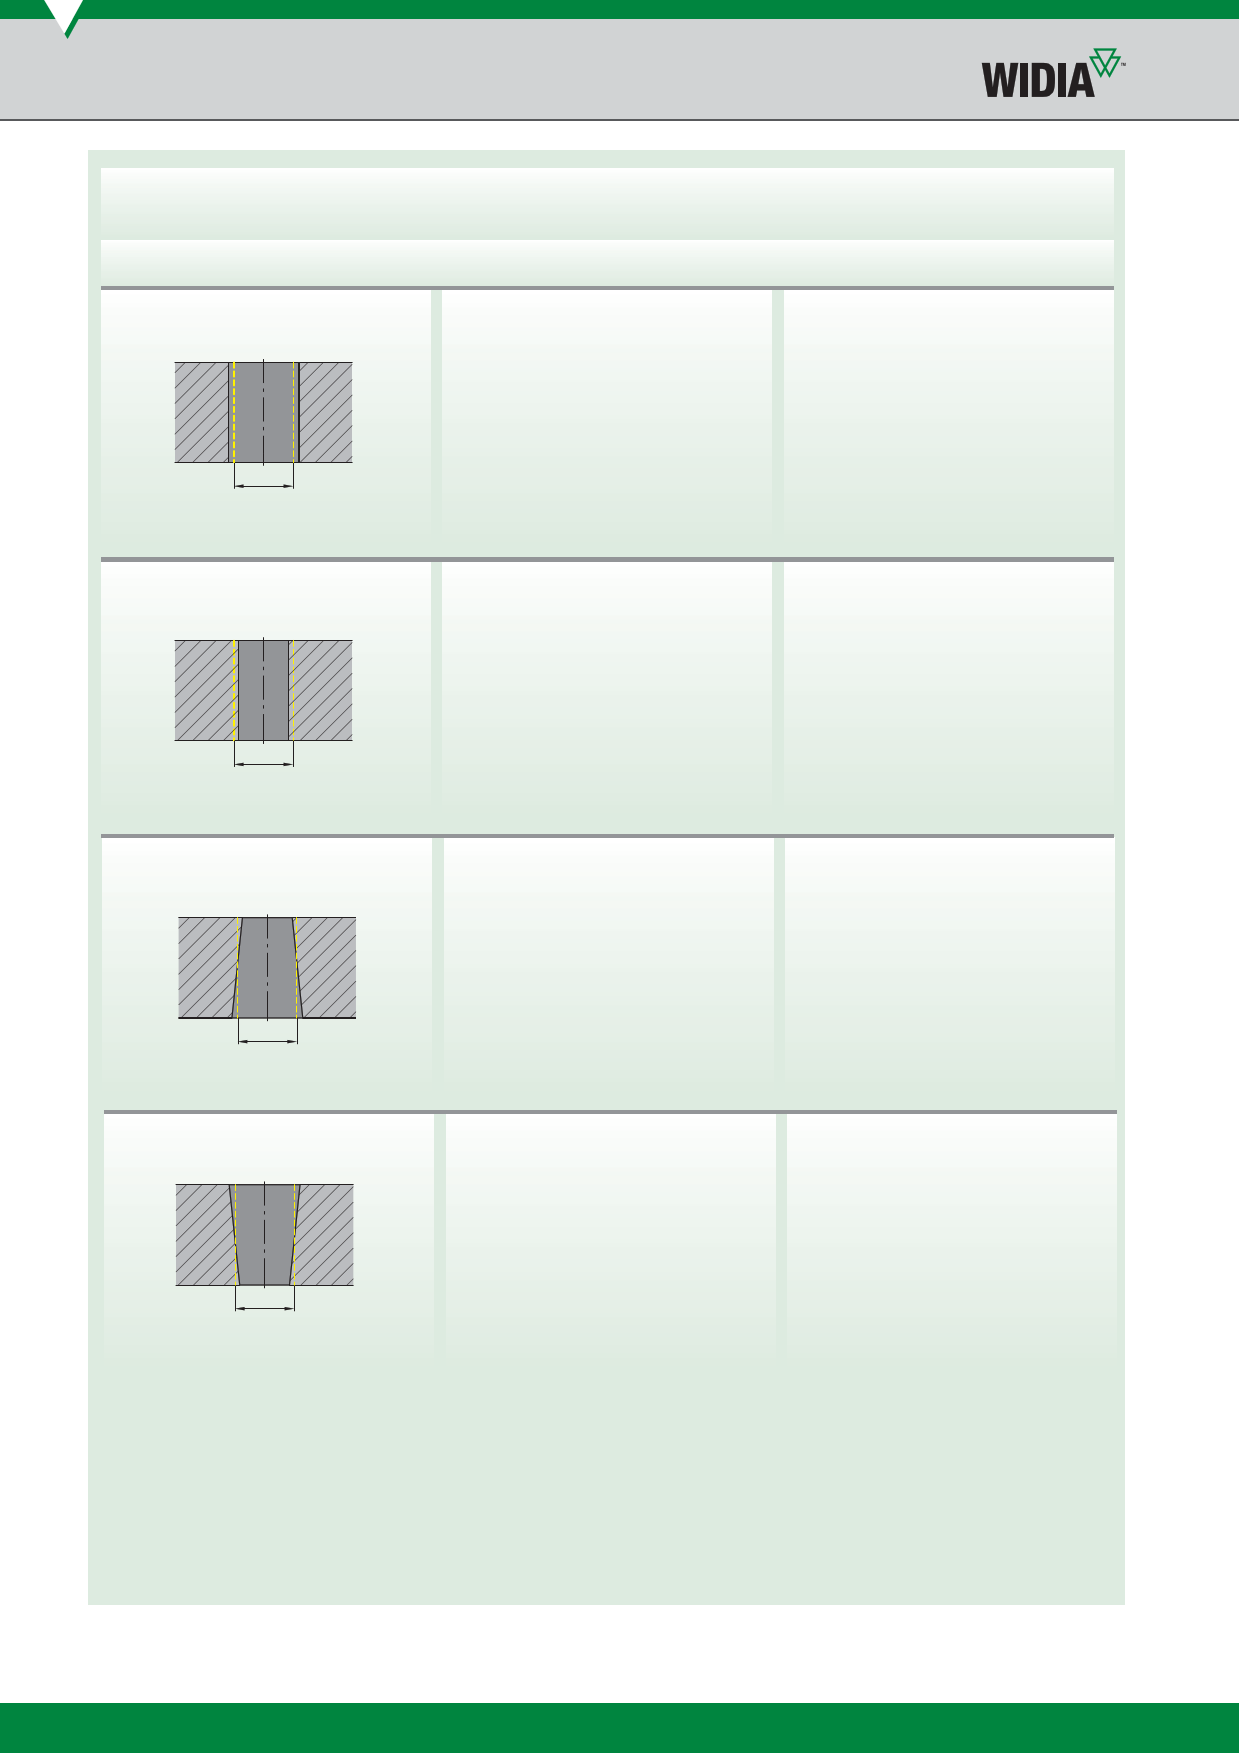
Hole diameter too large
Nom diameter
Hole diameter too small
Cause
1. Reaming tool running out of centre.
2. Concentricity of pilot hole and ream
machining unsatisfactory.
3. Built-up edge.
4. Unsuitable cooling lubricant.
5. Reaming tool diameter too large.
Possible Remedy
• Use equalising adaptor.
• Re-align, use floating head.
• Change cooling lubricant.
• Change cutting speed.
• Measure reamers and
send for repairs.
1. Reamer worn.
2. Unsuitable cooling lubricant.
3. Reaming allowance too small.
• Replace and refit tool.
• Change cooling lubricant.
• Increase reaming allowance.
Nom diameter
Conical hole profile wider towards drill runout
1. Concentricity of pilot hole and
reaming unsatisfactory.
2. Positioning accuracy of pilot hole
to reaming.
• Re-align, use equalising adaptor.
• Correct positioning accuracy.
Nom diameter
Conical hole profile wider at drill entry point
1. Concentricity of pilot hole and
reaming unsatisfactory.
2. Reaming tool skim cutting
with ledger.
• Re-align, use floating head.
• Securely clamp reaming tool axially.
Nom diameter
W32
zakaz@widiahanita.ru
www.widiahanita.ru
(continued)