
WIDIA - Полный каталог инструмента - 2017
Technical Information
Forming Taps
для размещения заказа - zakaz@widiahanita.ru
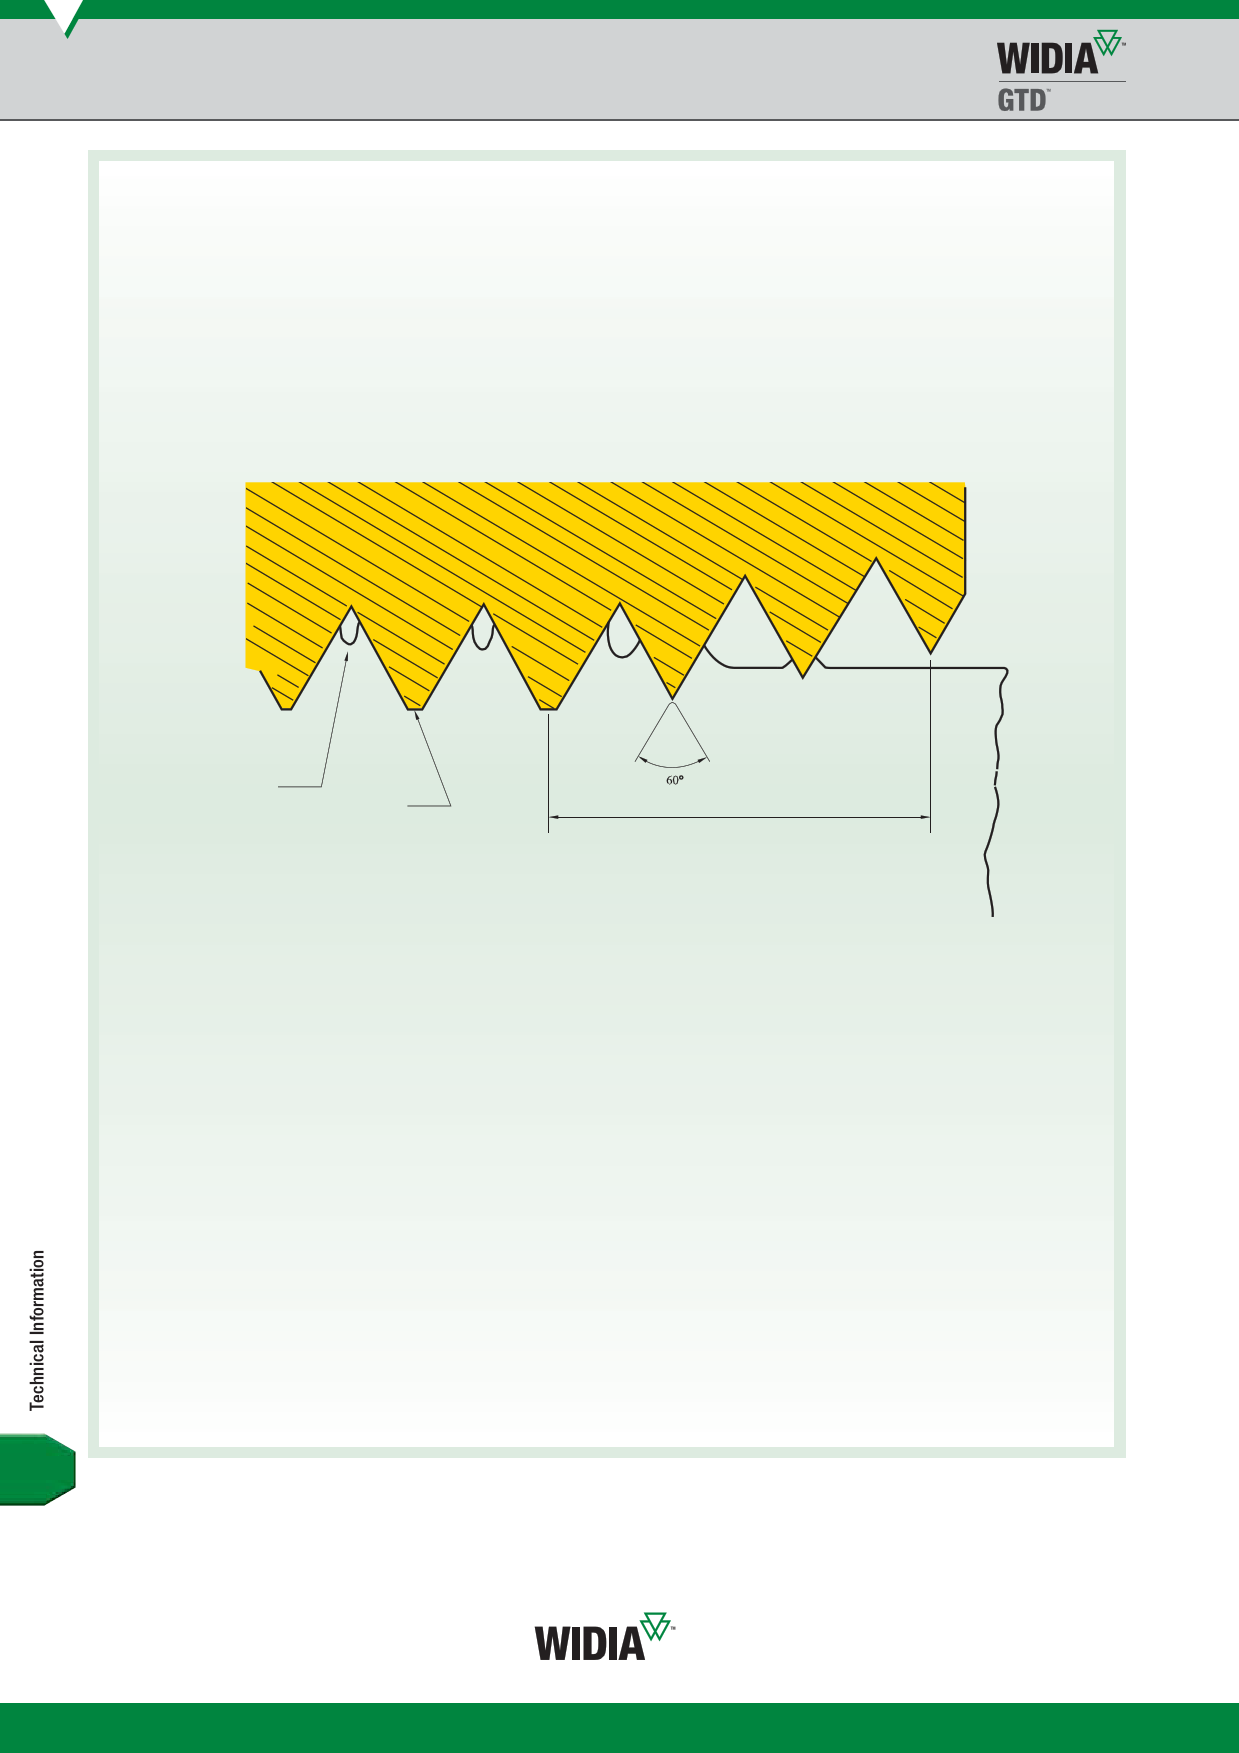
Unlike cutting taps, which remove material, forming taps generate an internal screw thread
by displacing material and forming it into the V-shaped thread. A common misconception
is that a thread rolling action occurs. Instead, the threads are formed over the tapered
entry section of the tap as the tap rotates into the hole. A succession of deeper
penetrating lobes over the entry plastically displaces material radially between the tap’s
thread flanks until the entry length is reached. At this point, the thread is fully formed at
the correct thread height.
Developed
Crest
Thread
Root
Tapered End
Forming taps have numerous advantages over cutting taps. The
most obvious advantage is that forming taps do not create chips.
There are no chip removal problems. Bird nesting is a situation
that occurs when chips wrap around the shank of spiral-fluted taps
when tapping blind holes in long chipping materials. Forming taps
help this to be avoided. Since forming taps avoid this problem,
they are stronger and more resistant to breakage. Another
misconception is that forming taps produce stronger threads.
Although the forming process strain hardens the thread flanks,
it has very little effect on the major diameter, the location where
internal threads strip.
Forming taps can only be used in ductile materials. Due to
increased friction relative to cutting, forming taps require higher
torque than cutting taps. In some situations, oil-based lubrications
are required, and this might not be convenient on CNC machining
centres that use water soluble coolant. In this situation, the
lubricant concentration should be increased.
Since forming taps displace material, larger diameter pre-tap holes
are required. This is especially important when converting from
cutting taps to forming taps. If a cutting tap hole size is used, the
displaced material will over-fill the tap’s threads and breakage will
result. Please consult hole size charts for forming taps.
Y102
zakaz@widiahanita.ru
www.widiahanita.ru