
WIDIA - Полный каталог инструмента - 2017
(continued)
Wrong
для размещения заказа - zakaz@widiahanita.ru
Solid Carbide Drills
General Application Instructions
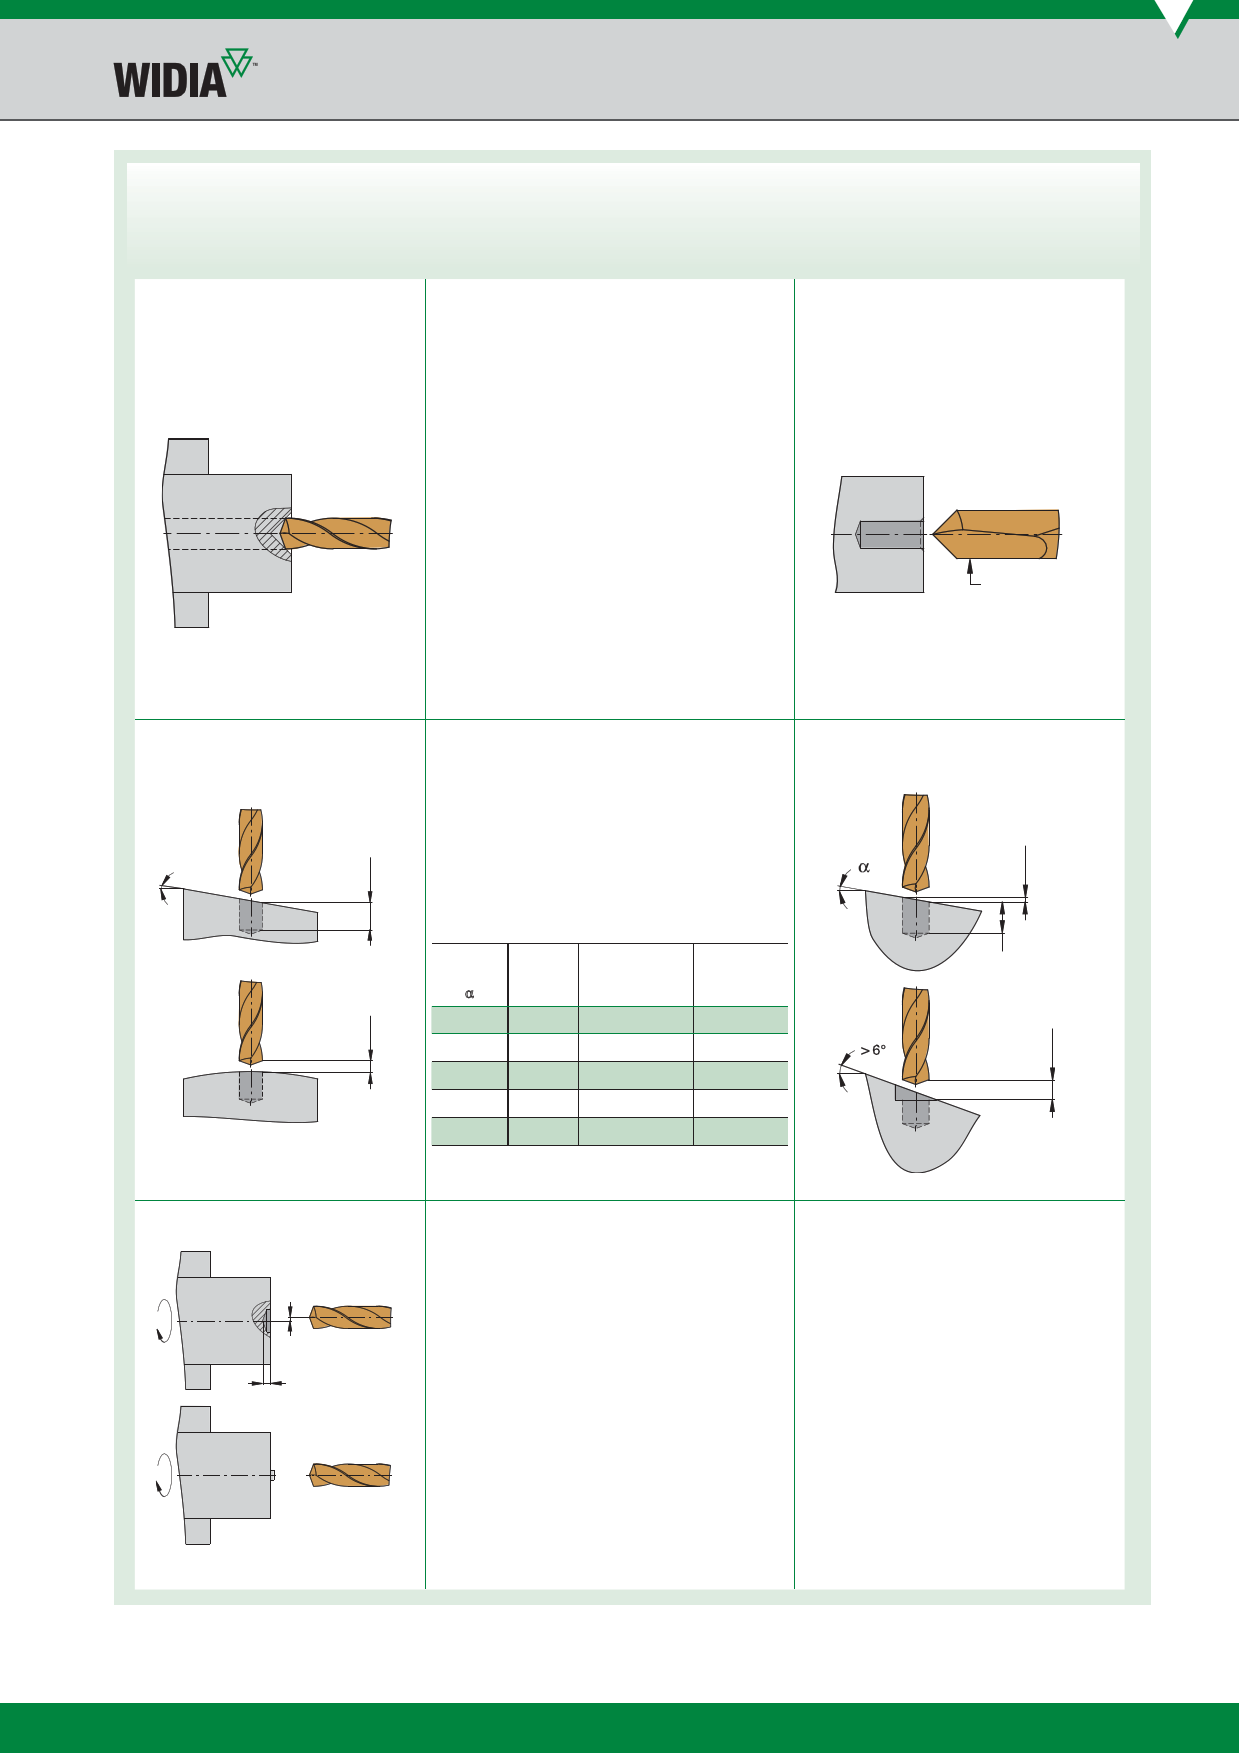
Drilling and Chamfering
Drill into the solid first, then chamfer.
Correct
Wrong
>1°
Wrong
[
100% feed
Drilling on Inclined or Rounded Surfaces
When drilling on inclined or curved surfaces, use a lower
feed than the standard value. The reduction of feed
required is dependent on the inclination angle of the
workpiece surface and the drill type (see table).
Correct
chamfer tool
reduced feed
reduced feed (% of standard value)
no premachine
inclination
_
1°
3xD
100%
5xD
Long
80%
<5 x D
premachine
2° 80–50% 80–50% premachine
3° 65%
50% premachine
4° 50% premachine premachine
[
6° 30% premachine premachine
Premachining is usually done with an end mill operation.
100% feed
premachine
0,025mm
Drilling on Turning Machines
When drilling on turning machines, the drill must be on
centre. The tolerance range of the centre position should
not exceed ±0.025mm. On bar-turning lathes, do not drill
into centre stub or bur. Cut-off tools must be mounted
precisely to eliminate centre stub or bur. Do not drill into
pre-existing holes.
Hole Depths Greater than 3 x D
Hole depths that are deeper than three times the
drill diameter may require a speed reduction. A
15% lower speed is suggested.
[
zakaz@widiahanita.ru
www.widiahanita.ru
T145