
WIDIA - Полный каталог инструмента - 2017
Solid Carbide Drills
General Application Instructions
для размещения заказа - zakaz@widiahanita.ru
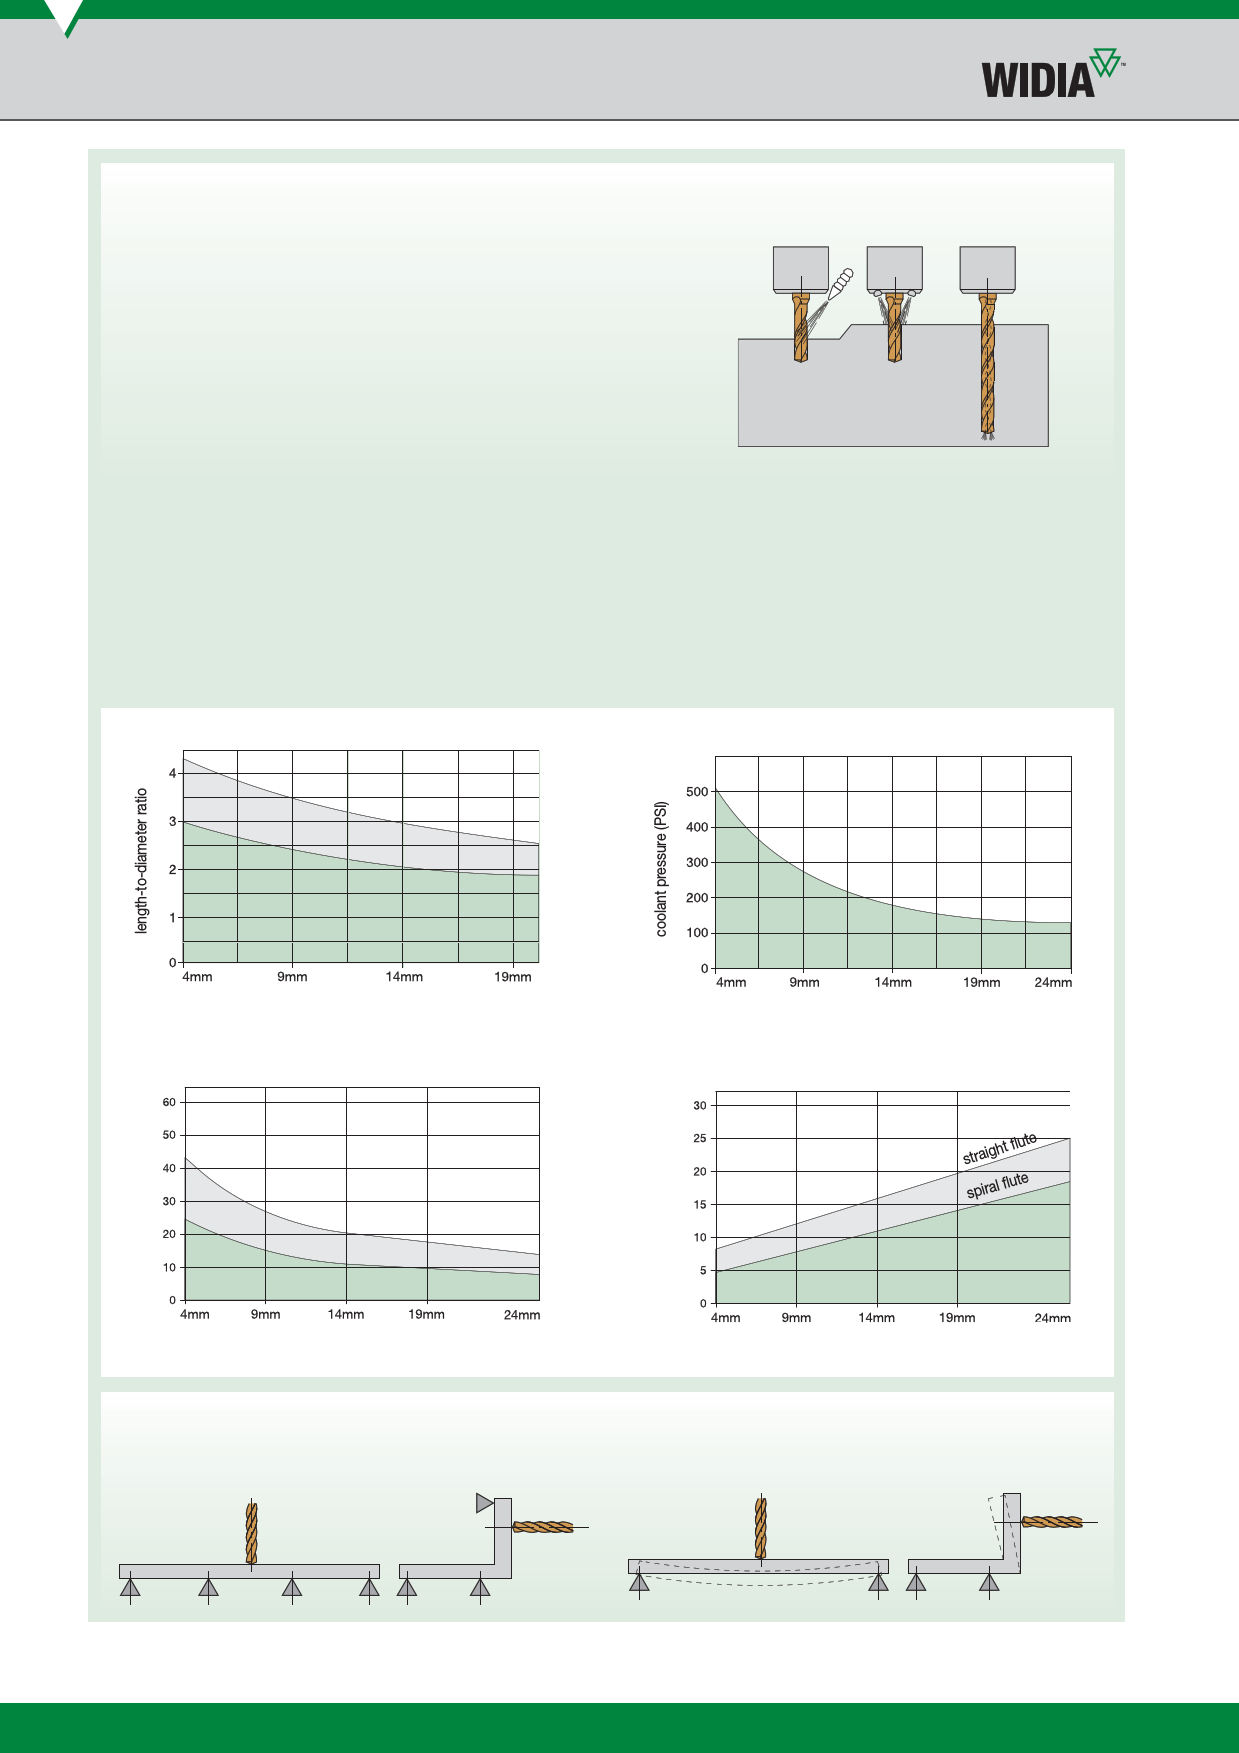
Coolant
• To optimise their performance, drills must be adequately cooled. With the
proper coolant flow, better tool life and higher maximum effective cutting
speeds can be achieved.
• If not properly cooled, the drill will heat up rapidly. This causes the drill
diameter to expand, which in turn may cause the drill to seize inside
the hole.
• Solid carbide drills with internal coolant channels require deeper drilling
depths to be effective. The higher the coolant pressure, the better the
drilling results. Drill life and hole quality improve with ample coolant flow.
• When using drills without internal coolant flow, try to get at least one
coolant jet as parallel to the drill as possible.
• For short-hole applications, drills without internal coolant may often provide
better tool life. The tool is more solid, and it does not suffer from thermal
shock at the cutting edge.
• It is important to use high coolant concentration to provide lubricity, which
will aid in tool life, chip evacuation, and finer surface finishes.
• High-pressure coolant, either through the tool or through a line adjacent
and parallel to the tool, should always be considered for increased tool life
and production.
• Do not use multi-coolant lines. Use one line with 100% of the flow capacity
to evacuate the chips from the hole.
Coolant requirement for carbide drills
Recommended pressure
internal coolant only
high-pressure flood coolant
flood
drill diameter
Recommended coolant flow volume V [l/min]
straight flute
spiral flute
Recommended pressure
favourable pressure values
coolant pressure too low
drill diameter
Recommended coolant pressure p [bar]
straight flute
spiral flute
drill diameter
drill diameter
Workpiece Rigidity
Because solid carbide drills have much higher penetration rates, it is important that the workpiece has adequate support.
correct
incorrect
T146
zakaz@widiahanita.ru
www.widiahanita.ru