
WIDIA - Полный каталог инструмента - 2017
для размещения заказа - zakaz@widiahanita.ru
Solid Carbide Drills
General Application Instructions
problem
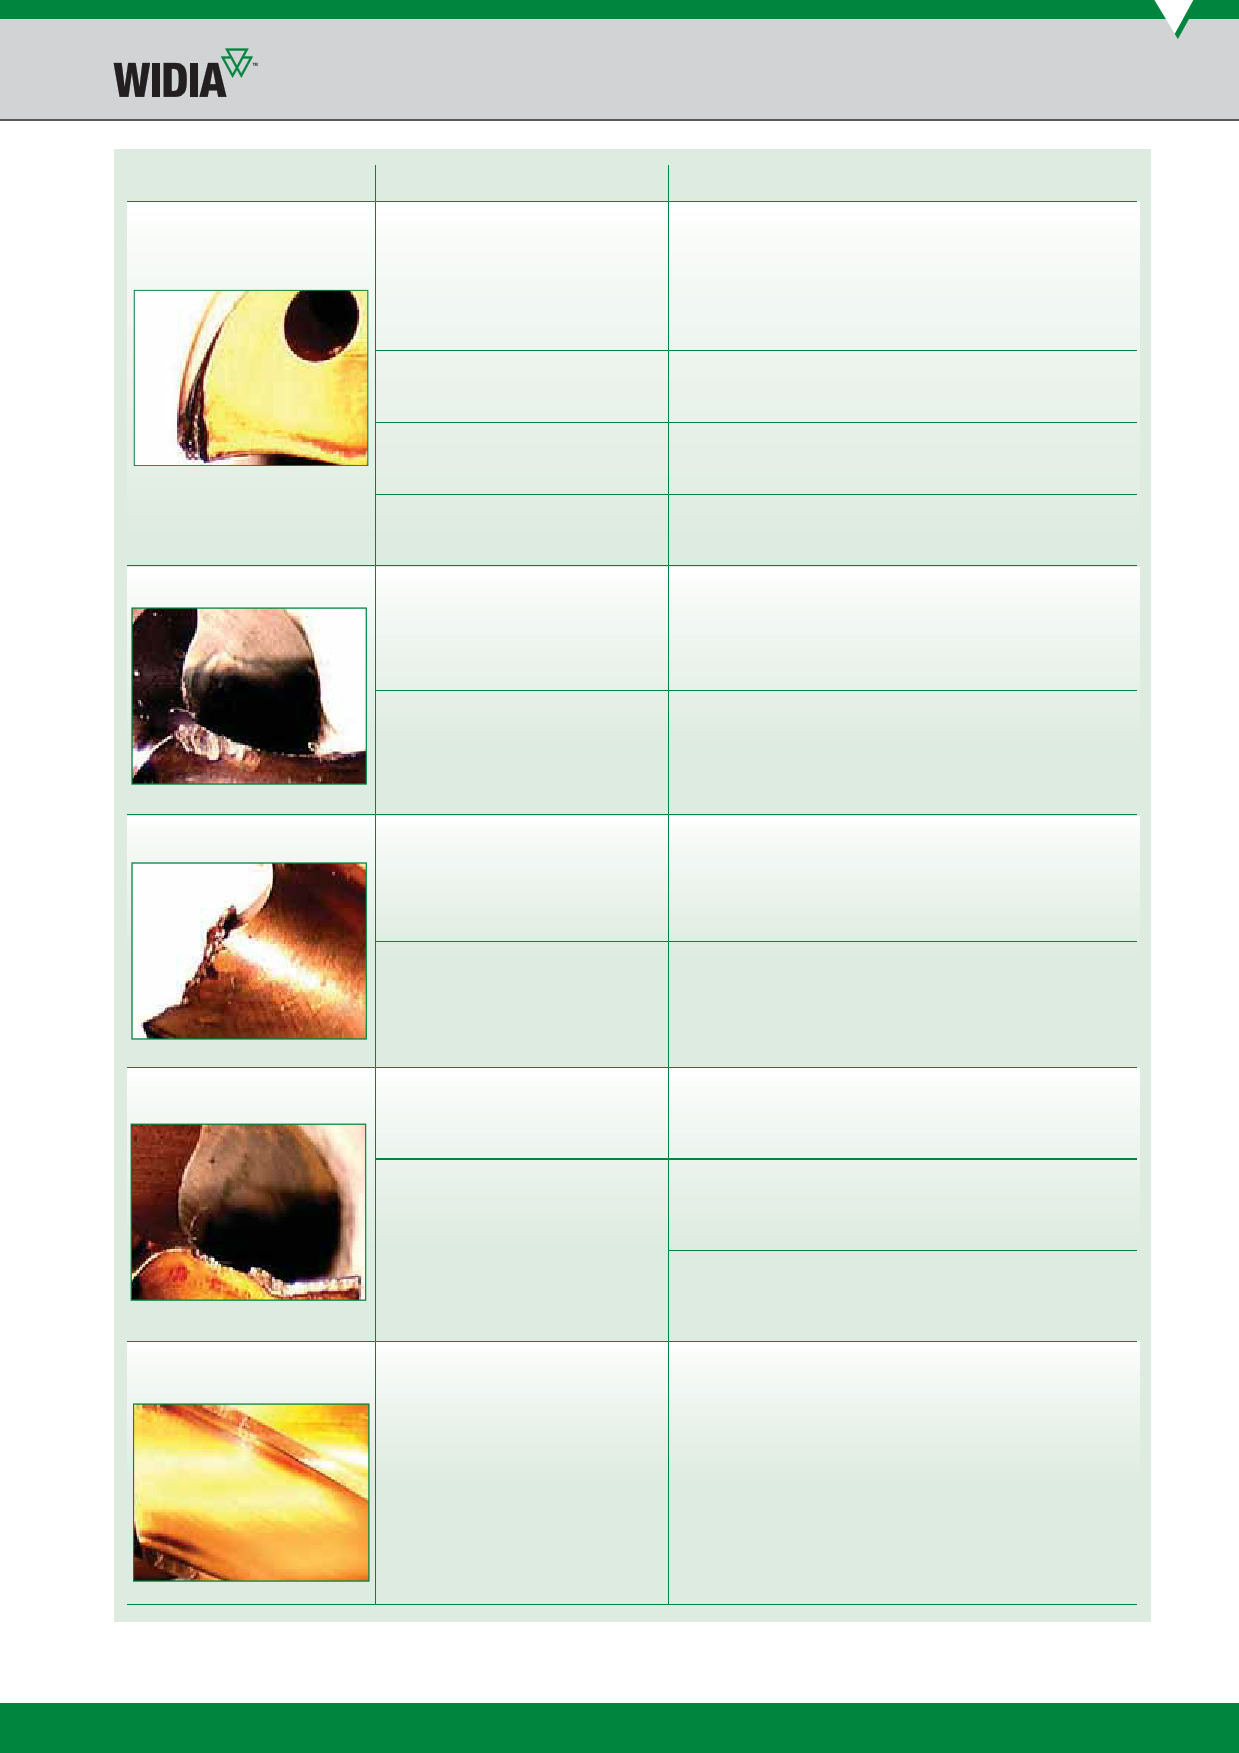
heavy wear on the cutting corners
source
insufcient coolant
solution
• Check cooling lubricant. In the case of internal coolant supply,
increase coolant pressure. In the case of external coolant supply,
adjust positioning of coolant jet. Cool from both sides.
splintering on the chisel edge
workpiece movement
wrong drill
cutting conditions
clamping chuck
• Stabilise workpiece chucking and check stability of machine tool.
• Check drill type, drilling depth, cooling system,
and workpiece material.
• Reduce cutting speed; increase feed.
• Check clamping accuracy. Use hydraulic clamping
chuck or high-precision chucking system.
cutting conditions
• Decrease feed; increase speed.
built-up edge
insufcient coolant
cutting conditions
• Check cooling lubricant. In the case of internal coolant supply,
increase coolant pressure. In the case of external coolant supply,
adjust positioning of coolant jet. Cool from both sides.
• Increase speed 20–30%.
splintering on the cutting edges
clamping chuck
cutting conditions caused
by built-up edge
• Check clamping accuracy and torque transmission. Use hydraulic
clamping chuck or high-precision chucking system.
• Check cutting values,and possibly increase cutting speed.
• Examine regularly for built-up edge.
thermal checking/comb cracking
cutting conditions
• Adapt coolant and cutting conditions to reduce thermal shock.
zakaz@widiahanita.ru
www.widiahanita.ru
T147