
WIDIA - Полный каталог инструмента - 2017
High-Performance Thread Mills
CNC Programming Instructions
для размещения заказа - zakaz@widiahanita.ru
Drill Thread Mill GTM41 • Left Hand
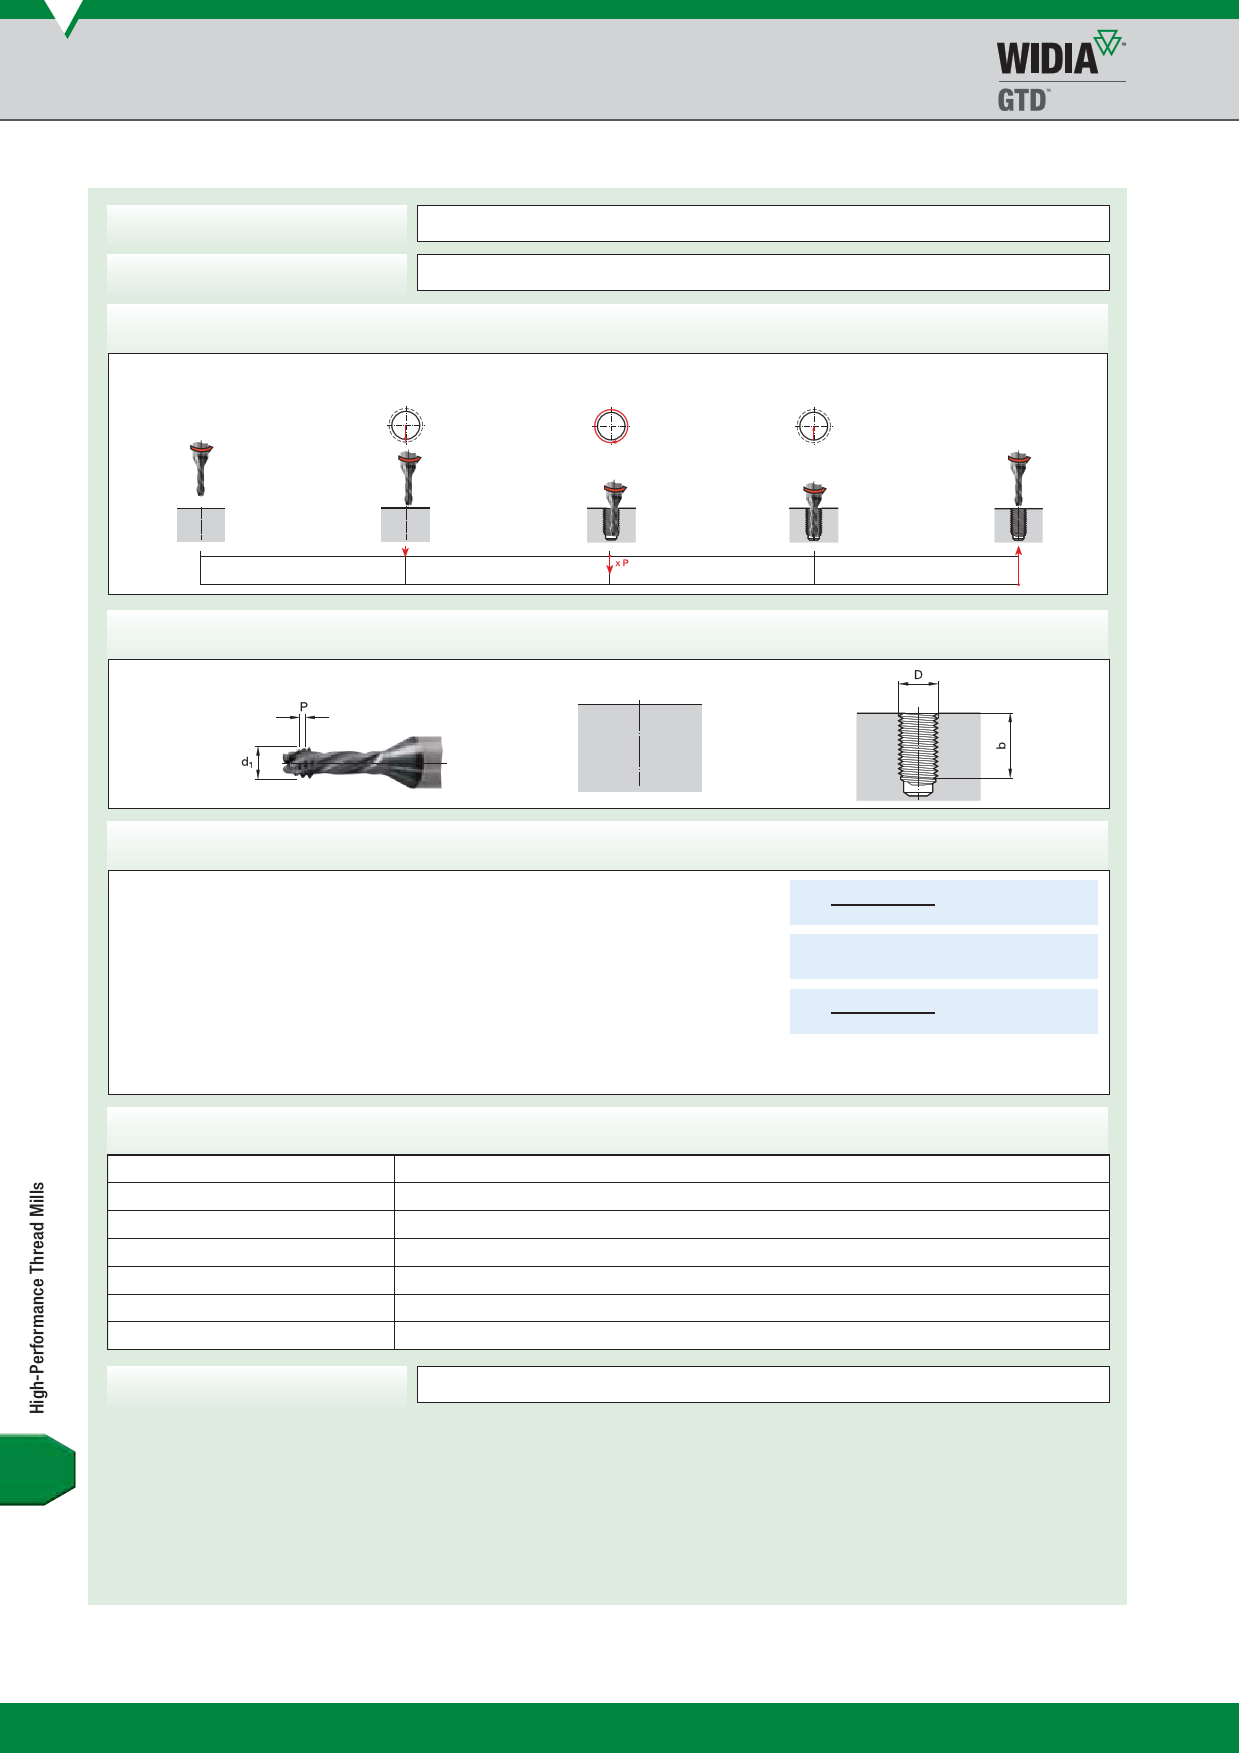
Preparation
Process Principle
Cycle
Positioning
None
Milling thread and core hole, countersinking (climb milling)
Moving sideways to
the starting point
Thread milling
(anti-clockwise)
Exit
Returning to
positioning level
Required Specication Values
Example
Size — M10-6H
Thread diameter D.........................................10mm
Pitch ............................................................. 1,5mm
Core hole diameter D1 ..................................8,5mm
Material — TiAl6V4 titanium
Grade — WU16PV
Tool — GTM41 Left Hand
Catalogue number ................................................GTM415005
Number of teeth Z..................................................................4
Tool
Tool
draiadmiuestceor md1p.e..n.s..a..t.i.o..n...k..1.........................................................................0.7,0,785mmmm***
Tool radius to be programmed2 ............................3,795mm***
Thread depth b ..............................................................20mm
Cutting speed vc..................................................... 100 m/min
FNeuemdb(emrilolifntgu)rnfzs.5.............................................................................................0..,.0..3...m...m.../.t.o..o1t7h
*(measured on the cutting pat)
**(0.01 x D)
***(1/2 d1 - k)
N = Vc • 1000
d1 • /
vf = fz • Z • n
S = 4109
F
=
493
(contour)
N = vf contour • (D-d1)
D
F = 111
(centre point)
Program to DIN 66025 (climb milling, on the contour, incremental)
Positioning the tool
Incremental programming
Moving sideways to the starting point
Thread milling
Repeat thread milling
Exit
Retracting tool to positioning level
N 10 G 54 G 90 G 00 X…
N 20 G 91
N 30 G 42 G 01 X 0 Y-5
N 40 G 02
…5
X0 Y0
N 50 G 40 G 01 X 0 Y 5
N 70 G 90 G 00 Z 2
Y… Z 1.500
F 493 (contour)
Z-1.500
I0
S 4109
T01 2 M04
[F 111] 4 (centre point)
J 5.000
Cutting time th
68.8 seconds
NOTES:
1 The cutter radius measured over the tooth crests of the threaded part must be reduced by the amount of the cutter radius compensation. This is necessary to achieve a depth of cut to the middle
of the 6H/ISO2 nut tolerance. Please note, however, that this also depends on the radial deection of the tool (tensile strength of the material, projecting length of the tool).
2 The cutter radius to be programmed is normally included in the tool memory.
3 The thread depth b must be divisible by the thread pitch P.
4 The feed values in brackets must be used for controllers, which do not calculate the centre point feed themselves.
5 Set N40 must be repeated with the number of threads. Repetitions N = thread depth b/pitch P (rounded up to the nearest integer).
Y82
zakaz@widiahanita.ru
www.widiahanita.ru