
WIDIA - Полный каталог инструмента - 2017
для размещения заказа - zakaz@widiahanita.ru
High-Performance Thread Mills
CNC Programming Instructions
Drill Thread Mill GTM31
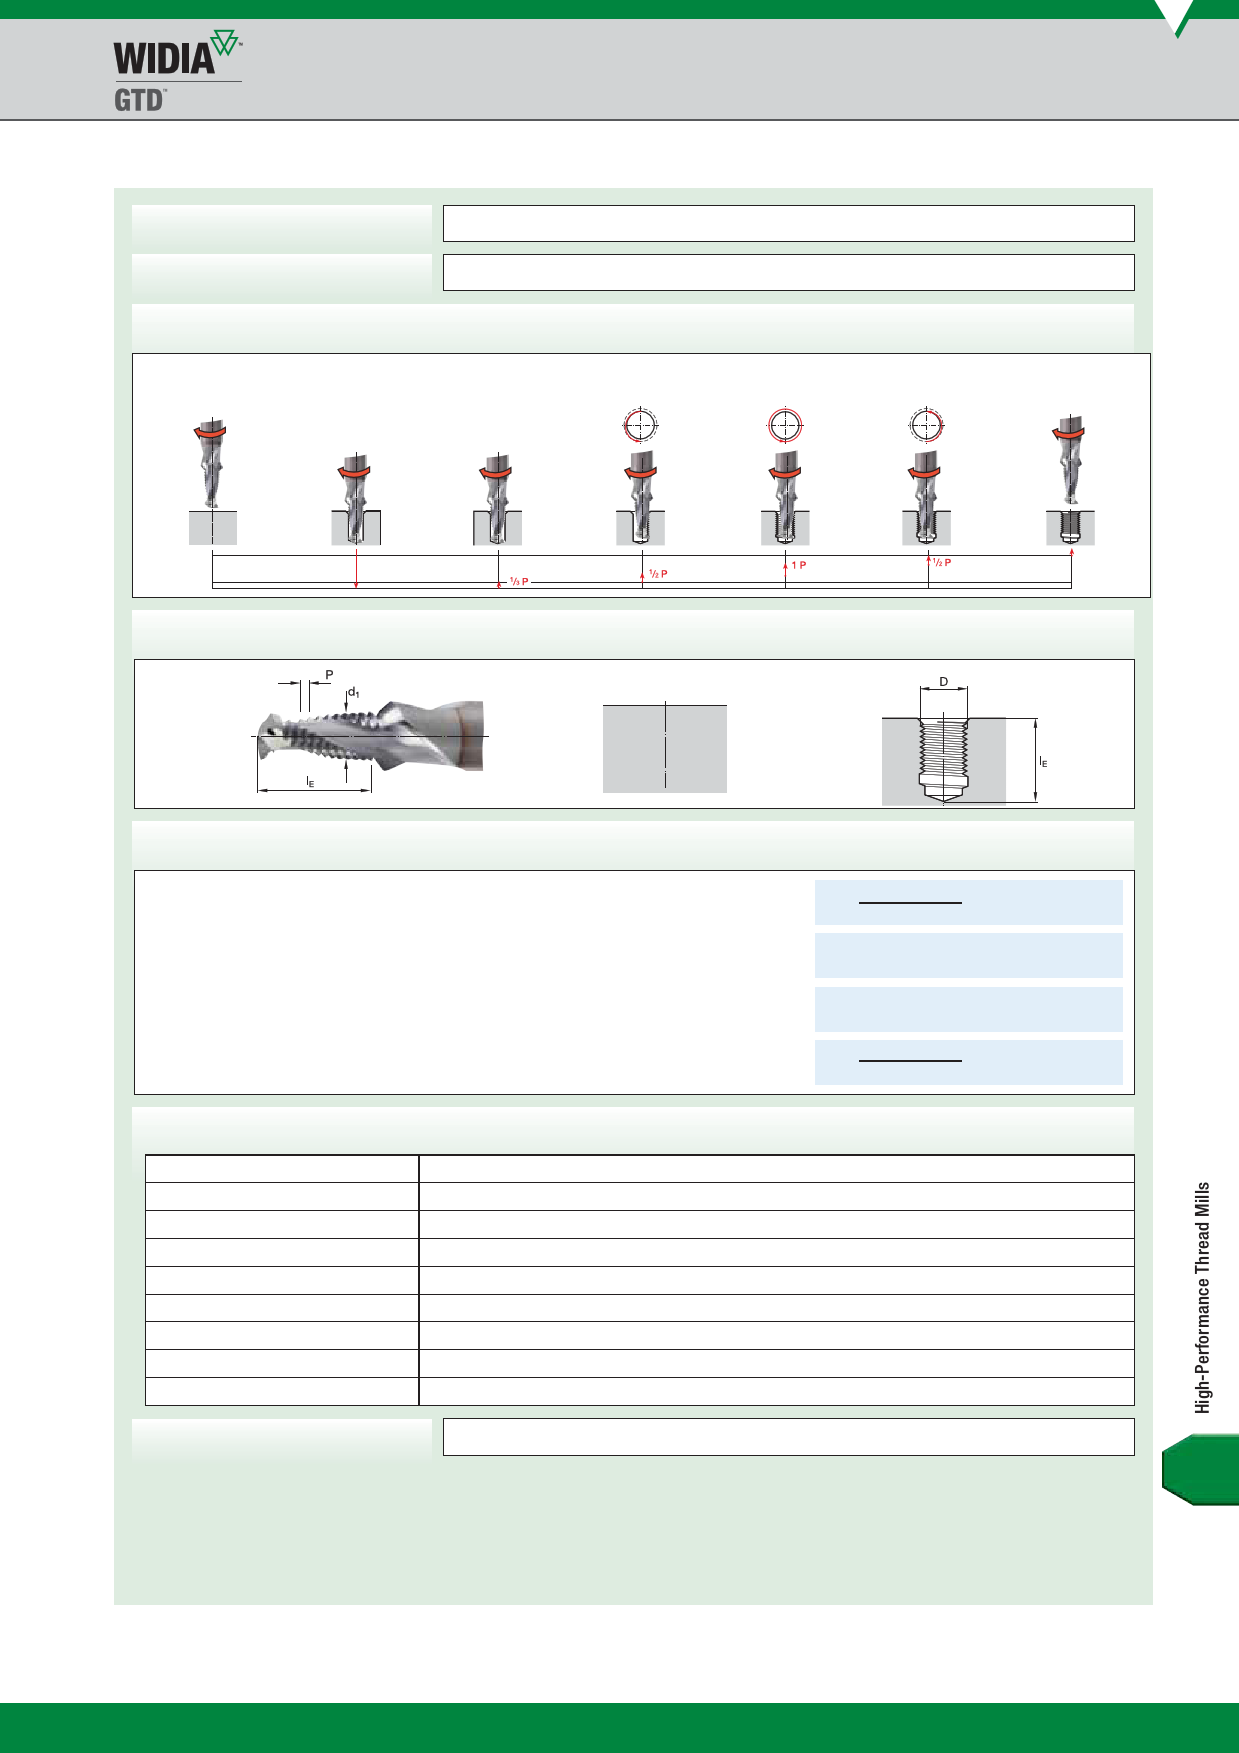
Preparation
Process Principle
Cycle
Positioning
Drilling and
countersinking
Drilling of thread hole
Drilling, countersinking, thread milling (climb milling)
Raise
Run-in loop for
thread milling
Thread milling
Run-out loop
Returning to
positioning level
Required Specication Values
Example
Size — M10-6H
Thread diameter D.........................................10mm
Pitch ............................................................. 1,5mm
Core hole diameter D1 ..................................8,5mm
Material — Grey cast iron
Grade — WU12PV
Tool — GTM31
Catalogue number ................................................GTM315005
Number of teeth Z..................................................................2
Tool
Tool
draiadmiuestceor md1p.e..n.s..a..t.i.o..n...k..1.............................................................................0.8,1,2mmmm***
Tool radius to be programmed2 ...................................4mm***
Countersink depth ls.................................................19,11mm
Cutting speed vc..................................................... 250 m/min
Feed (countersinking fs..........................................0,25 mm/U
Feed (milling) fz .................................................. 0,1 mm/tooth
*(measured on the cutting part)
**(0.01 x D)
***(1/2 d1 - k)
N = Vc • 1000
d1 • /
vs = fb • n
vf = fz • Z • n
S = 9709
F
=
2427 (drilling,
countersinking)
F
=
1942
(contour)
vf contour • (D-d1)
vf = D
F = 350
(centre point)
Program to DIN 66025 (climb milling, on the contour, incremental)
Positioning the tool
N 10 G 54 G 90
G 00
X…
Y…
Z 2 S 9709 T01 2
M03
Drilling and countersinking
N 20 G 91 G 01 Z-21.110 F 2427 (drill, countersink)
Raise
N 30 G 01 Z 0.500
Moving sideways to the starting point N 40 G 41 Y-4.250
F 971 (milling, 1/2 contour)
[F 175] 3 (1/2 centre point)
Run-in loop in arc
N 50 G 03 X 0
Y 9.250 Z 0.750
I0
J 4.625
Thread milling
Run-out loop in arc
N 60 G 03 X 0
Y 0 Z 1.500 I 0 J -5.000
N 70 G 03 X 0 Y-9.250 Z 0.750 I 0 J- 4.625 F1942 [F 350] 3 (centre point)
Exit
N 80 G 00 G 40
X 0 Y 4.250
Retracting tool to positioning level
N 90 G 90 Z 2
Cutting time th
2.3 seconds
NOTES:
1 The cutter radius measured over the tooth crests of the threaded part must be reduced by the amount of the cutter radius compensation. This is necessary to achieve a depth of cut to the middle
of the 6H/ISO2 nut tolerance. Please note, however, that this also depends on the radial deection of the tool (tensile strength of the material, projecting length of the tool).
2 The cutter radius to be programmed is normally included in the tool memory.
3 The feed values in brackets must be used for controllers, which do not calculate the centre point feed themselves.
zakaz@widiahanita.ru
www.widiahanita.ru
Y83